Home / Products / KS

Hot chamber · horizontal

KS series · 38 to 88 tonnes

Compact hot-chamber machines for zinc and magnesium. The gooseneck sits in the melt and the shot chamber fills by itself, which is what makes the short cycle possible.

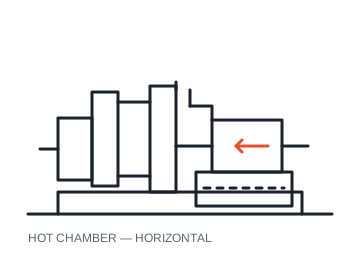
Hot-chamber die casting machine schematic

Built for small parts at speed

On a hot-chamber machine the shot chamber and plunger are immersed in the molten alloy. The plunger travels down, the metal is forced through the gooseneck and the nozzle into the die, and the chamber refills on the return stroke. There is no ladling step, so the cycle is short and repeatable.

That only works below about 650 °C. Zinc and magnesium sit comfortably inside that limit; aluminium does not, which is why there is a separate cold-chamber range.

Where the KS series fits

  • Zinc lock bodies, zipper sliders, buckles, hardware and decorative parts
  • Magnesium covers and small housings where weight matters
  • Shielding cans and small connector shells

Models

ModelClamping forceAlloysTypical use
KS-3838 TZinc, magnesiumSmall hardware, sliders, decorative
KS-5050 TZinc, magnesiumLock bodies, buckles, brackets
KS-8888 TZinc, magnesiumLarger housings, multi-cavity small parts

Die height, platen size, shot weight and tie-bar spacing are confirmed per model on the quotation — send us the die drawing and we will check it against the machine.
Standard configuration

  • Hydraulic clamping with gear-type die height adjustment
  • Reinforced injection system with large-bore logic valve
  • Low-oil and low-pressure alarms protecting the clamping system
  • Electrical control configured to CE safety practice; touchscreen or dial control
  • Furnace options: diesel, gas, electric or electric-resistance crucible
CE marking is not held on every configuration. Tell us the destination market and we will confirm what documentation the machine can be supplied with.